Explore our export-ready, CE-certified translucent natural stone luminaires designed for luxury hospitality, high-end residential, and commercial specification.
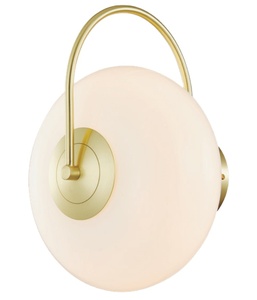
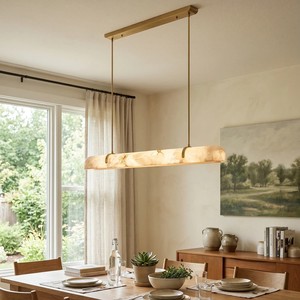
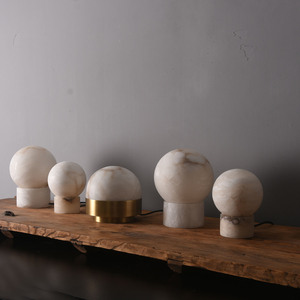
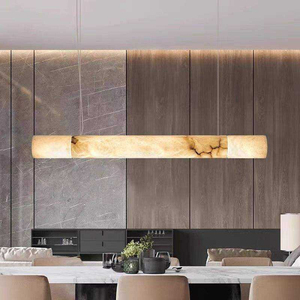
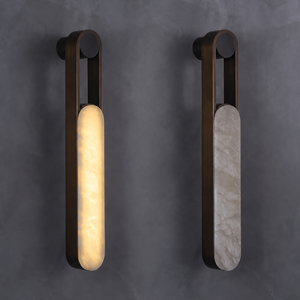
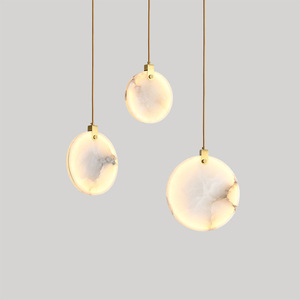
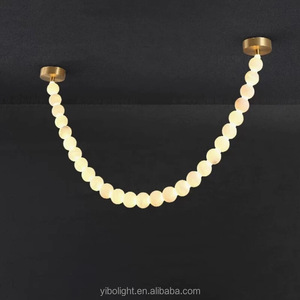
Combining 50 years of heritage in precision metal fabrication with state-of-the-art CNC alabaster stone sculpting to support global B2B procurement networks.
As a leading CE Certified Alabaster Lamp Manufacturer & Factory network, our enterprise commitment revolves around preserving the structural and optical integrity of natural alabaster stone (calcium sulfate dihydrate). Unlike synthetic acrylic or poured resin imitations that degrade under continuous LED thermal exposure, authentic quarried alabaster possesses a crystalline lattice structure that naturally diffuses luminous flux while retaining dimensional stability over decades.
"Resin copies flatten illuminate tone and yellow over time under thermal stress. Genuine quarried alabaster diffuses light with volumetric depth, transmitting warm 2700K–3000K Kelvin warmth through unique mineral veining that no automated chemical process can replicate."
| Evaluation Parameter | Natural Quarried Alabaster (Our Factory) | Faux Acrylic / Polymer Resin |
|---|---|---|
| Composition & Origin | Quarried natural calcium sulfate dihydrate stone | Petroleum-derived synthetic polymer resins |
| Thermal Endurance | Stable up to 180°C; zero outgassing or deformation | Deforms/softens above 65°C; potential thermal discoloration |
| Refractive Index & Diffusion | Multi-crystalline volumetric refraction (Warm ambient diffusion) | Surface-level light scattering (Flat optical dispersion) |
| Environmental & Aging Stability | Permanent UV resistance; non-yellowing mineral structure | Degrades under continuous UV and LED blue-light exposure |
| Safety Certification | Fully EN 60598-1 non-combustible material compliance | Variable flame retardancy; requires added chemical retardants |
Architects, lighting specifiers, and procurement directors must evaluate stone selection based on density and mineral purity. Our manufacturing facility sources raw alabaster blocks directly from historic quarry reserves, subjecting each raw slab to ultrasonic testing to identify internal fissures prior to 5-axis CNC machining, lathe turning, and hand-applied wax polishing.
Our vertically integrated OEM/ODM plant combines traditional metal patination with modern photometric engineering to deliver seamless B2B contract solutions.
We eliminate installation compromises by manufacturing overall drop lengths, stem dimensions, backplate scaling, and shade profiles to your exact CAD site specifications before entering production.
Every luminaire assembly undergoes rigorous dielectric withstand testing, grounding continuity verification, and photometric profiling to meet Low Voltage Directive (LVD 2014/35/EU) and EMC requirements.
We craft non-ferrous housings from solid heavy-gauge brass, copper, and bronze. Unlike plated sheet metal, our structural metalwork patinas gracefully over time and resists coastal salt air corrosion.
Custom reinforced wood-crate packaging designed specifically for fragile alabaster transportation ensures safe transit to project sites across Europe, North America, the Middle East, and Asia-Pacific.
Our dedicated engineering office provides technical shop drawings, photometric IES files, physical finish finish samples, and stone vein pre-selection imagery before final manufacturing release.
As global luxury hospitality brands and high-end residential developers shift toward biophilic design and organic architectural textures, the demand for natural stone luminaires has grown exponentially. As a dedicated CE Certified Alabaster Lamp Manufacturer & Factory, we have identified three macro procurement trends redefining global specification standards:
Modern interior environments demand dynamic lighting transitions. Future-ready alabaster luminaires are no longer fitted with simple fixed-CCT LED modules. Instead, enterprise buyers are specifying custom light engines supporting Warm-Dimming technology (3000K down to 1800K) paired with advanced control interfaces including DALI-2, 0-10V, and TRIAC/ELV dimming drivers. Because alabaster stone possesses a warm natural hue, warm-dimming technology highlights the rich translucent veins during nighttime scene settings without introducing high-frequency flicker or acoustic hum.
Recent architectural trends favor continuous linear stone profiles over traditional multi-arm chandeliers. Kitchen island pendants and executive boardroom ceiling lights now incorporate continuous CNC-machined alabaster tubes measuring up to 1500mm in length. Achieving structural integrity in long-format stone requires specialized internal steel tension rods and precision metal end-caps, engineering capabilities that separate specialized alabaster factories from generic assembly shops.
International procurement frameworks prioritize low VOC footprint, repairability, and circular material lifecycles. Real quarried alabaster paired with unlacquered hand-rubbed brass fits perfectly into sustainable building certifications (LEED v4.1 & WELL Building Standard). The absence of synthetic plastic laminates guarantees that components can be serviced, re-polished, or recycled indefinitely without generating hazardous waste.
Our 6-stage quality control process guarantees structural safety, exact electrical tolerance, and pristine surface finish for international commercial distribution.
| Manufacturing Stage | Process Details | Quality Inspection Criteria |
|---|---|---|
| Stage 1: Stone Selection | Direct quarry extraction of high-translucency gypsum alabaster blocks. | Ultrasonic flaw detection; color tone matching & vein density grading. |
| Stage 2: Precision Sculpting | 5-axis CNC wet-milling, diamond lathe turning, and hand-sculpting. | Wall thickness tolerance within ±0.3mm for uniform light diffusion. |
| Stage 3: Metalwork Fabrication | Precision spinning, TIG welding, and hand-applied patination of solid brass/bronze. | Salt-spray testing (240 hours) & mechanical structural load testing. |
| Stage 4: Electrical Assembly | Integration of CE-marked LED PCB arrays, constant-current drivers, and heat sinks. | Dielectric strength test (1500V AC), grounding continuity check (<0.1Ω). |
| Stage 5: Photometric Testing | Integrating sphere & goniophotometer color rendering index assessment. | CRI > 92, R9 > 50, optical efficiency > 85 lm/W through stone. |
| Stage 6: Export Packaging | Custom molded drop-tested foam enclosure inside wooden crate framing. | ISTA 3A drop test & vibration simulation compliance. |
Key technical and logistical inquiries addressed for commercial buyers, architectural specifiers, and OEM importers.
Yes. All luminaires manufactured in our factory carry comprehensive CE certification adhering to the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility Directive (EMC 2014/30/EU). We provide complete CE declaration documentation, test reports, and RoHS compliance certification for seamless customs clearance and building inspection.
We utilize a proprietary multi-layer protective packaging system. Each stone component is wrapped in anti-scratch film, encased in high-density customized EPE foam molds tailored to the luminaire's exact geometry, and sealed inside heavy-duty double-wall corrugated cartons reinforced with solid wooden crate framing. Our packaging complies with ISTA 3A transit testing standards.
Absoltely. Over 70% of our production output involves custom engineering. Our internal engineering department works directly with architectural drawings, offering CAD shop drawing production within 48 hours, 3D modeling support, custom finish matching, and private label OEM branding (laser-engraved logo plates and custom packaging).
For standard catalog collections, our lead time is 15–20 days. Custom contract fixtures require 25–30 days depending on stone carving complexity and patination requirements. We support flexible MOQs for trade professionals, starting from low-volume project samples up to container-load commercial orders.
Because alabaster is a natural mineral, every cut piece displays subtle organic veining. To guarantee project harmony across multi-fixture installations, our factory provides a pre-assembly photo approval protocol, sending high-resolution images of matched stone panels for specifier approval before final assembly and dispatch.
Connect directly with our engineering sales team to request factory pricing, material samples, photometric IES files, or technical CAD consultations.