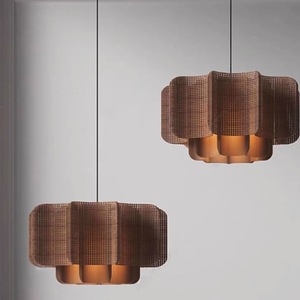
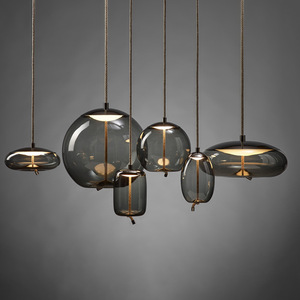
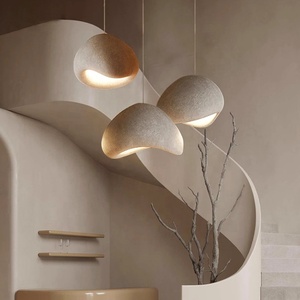
In modern architectural lighting, the integration of natural stone—specifically Spanish Alabaster, Travertine, and Cloud Marble—represents a profound shift from mass-market synthetic fixtures toward organic, biophilic luxury. As an established OEM/ODM stone chandelier manufacturer, our engineering workshop bridges the gap between raw geomorphic beauty and high-performance optoelectronic systems.
Unlike artificial resin imitations, authentic quarried stone possesses a microscopic crystal lattice that refractorially diffuses LED light across a broad color spectrum. This natural translucency eliminates harsh glare while preserving warmth. However, manufacturing large-scale stone chandeliers for hospitality lobbies, high-ceiling staircases, and luxury residential projects presents unique structural, thermal, and photometric challenges that require rigorous custom engineering standards.
Five-axis CNC water-jet diamond routing achieves consistent stone wall thickness down to 4mm ± 0.1mm, ensuring balanced light transmission without structural compromise.
Aircraft-grade stainless steel internal armatures and solid brass suspension hardware designed to carry up to 5x safety margin for seismic and structural building codes.
Custom extruded aluminum heat sinks dissipate LED thermal output away from delicate stone shades, guaranteeing a 50,000-hour LED lifespan without stone discoloration.
Modern interior designers are rejecting stark minimalist synthetics in favor of tactile, organic stone elements. Travertine wall sconces, Wabi-Sabi cloud stone pendants, and alabaster globe chandeliers provide the raw texture required for contemporary organic modernism. Sourcing authentic quarried stone ensures every unit features unique veining, delivering bespoke luxury for high-end hospitality projects.
Commercial lighting contracts increasingly demand smart connectivity. Our custom OEM manufacturing integrates universal dimming drivers (DALI-2, 0-10V, Phase-Cut, Zigbee, and Tuya APP Control) directly into canopy junctions. This allows hotel operators and estate owners to program dynamic circadian rhythm scenes through natural stone diffusers.
Enterprise buyers are prioritizing low total cost of ownership (TCO). Rather than glued single-body assemblies, our engineering process utilizes quick-release brass mechanical couplings and standardized LED light engines. In the event of maintenance, stone shades or LED modules can be swapped on-site without dismantling the entire chandelier structure.
| Technical Evaluation Criteria | Genuine Quarried Alabaster / Stone | Faux Resin / Acrylic Imitation | OEM Specification Advantage |
|---|---|---|---|
| Optical Refractive Index | 1.57 - 1.60 (Natural crystalline diffusion) | 1.49 (Static plastic refraction) | Authentic depth, zero LED hotspot glare |
| Thermal Resistance & Aging | Heat resistant up to 800°C; zero yellowing | Degrades & yellow under UV/LED heat over time | Infinite stone lifespan with replaceable LED engine |
| Acoustic & Density Feel | High density (2.3 g/cm³), luxury solid feel | Low density (1.1 g/cm³), hollow lightweight feel | Substantial weight creates premium tactile value |
| Unique Veining Authenticity | 100% unique natural mineral veining per shade | Repeated printed or cast pattern loops | Bespoke uniqueness for every hotel room or villa |
| Fire & Building Code Rating | Class A1 Non-combustible stone body | Combustible plastic (Requires chemical flame retardants) | Simplifies commercial building code compliance |
As a dedicated B2B manufacturer, our factory operates as an extended engineering laboratory for architects, interior designers, lighting specifiers, and OEM brand distributors worldwide. We streamline custom procurement through a rigorous 6-step project execution framework:
Our engineering team converts client sketches, mood boards, or BIM files into detailed 2D/3D CAD shop drawings, analyzing weight distribution, ceiling canopy mounting mechanics, and overall stem drop lengths.
Clients select raw stone slabs (Alabaster, Travertine, Marble) from our quarry inventory based on preferred veining density, color tone, and light translucency profile before machining begins.
High-precision multi-axis CNC machines cut, hollow, and polish the stone shades to exact wall thickness tolerances, followed by manual hand-finishing by master stone artisans.
Solid brass, bronze, or copper armatures undergo hand-applied patination (Unlacquered Antique Brass, Satin Nickel, Matte Black, or Aged Bronze) to match exact hardware samples.
Every custom chandelier undergoes full electrical safety testing (Hi-Pot, Grounding Continuity), IES photometric sphere testing, and continuous 48-hour burn-in inspection.
Fixtures are disassembled into modular components, suspended in custom-molded EPE foam, and encased in ISPM-15 compliant heat-treated wooden crates for international sea/air freight.
Structural safety is paramount. All large-scale OEM stone chandeliers (exceeding 25 kg / 55 lbs) are engineered with an independent internal structural load line. The electrical ceiling box supports zero load; instead, an aircraft steel cable or threaded steel rod attaches directly to the building's structural beam. We provide engineered mounting bracket templates and structural load calculations for local site engineering sign-off.
Yes. Every pendant and chandelier can be manufactured to your exact overall drop height, stem length, backplate dimension, and shade diameter. During the CAD review stage, our technical team calculates sightlines, ceiling heights, door clearances, and dining table proportions to ensure perfectly scaled installation.
Our lighting fixtures are manufactured to meet global regulatory standards. Depending on your destination market, we supply fixtures fully wired and certified to UL 1598 / CSA standards for North America, CE / EN 60598 for Europe and the UK, SAA for Australia, and SASO for the Middle East. Drivers are certified with IP ratings appropriate for dry, damp, or wet locations.
No. We use genuine quarried alabaster and travertine natural stone that has formed under high geological pressure over millions of years. Unlike synthetic resin, natural stone is completely stable under heat up to 800°C. Furthermore, our integrated aluminum thermal sinks ensure LED operating temperatures remain below 55°C, preventing heat stress or discoloration.
Following 2D/3D CAD drawing approval and finish sample confirmation, standard OEM sample prototyping requires 15 to 20 business days. Bulk production for commercial hospitality projects typically spans 30 to 45 days, depending on stone quarrying volume and total fixture complexity. Express air freight and consolidated sea freight shipping are fully supported.
While natural stone intrinsically features micro-variations in veining, we execute strict quarry batching. Slabs for a single project are cut from the same geological block layer. Before final assembly, shades are backlit, spectrophotometrically color-sorted, and photographed so specifiers can approve stone vein groupings before international shipment.
Partner directly with an established OEM stone chandelier factory. Our technical specification desk provides complete CAD drawings, physical stone/metal finish sample kits, photometrics, and factory-direct volume quotes within 24 hours.